
Rust Prevention & Lubricant Selection for Tropical Centrifugal Compressors

Tropical, monsoon and coastal regions feature ambient temperature above 30°C all year round, relative humidity consistently over 80%, and salt spray in nearshore sites. As high-speed rotating equipment, centrifugal compressors have impellers, main shafts, bearings, gearboxes and oil separators highly sensitive to moisture.
Many overseas projects in India, Indonesia, Egypt, Bangladesh and other regions face identical failures: units run normally while condensation forms inside chambers after cool-down; lube oil emulsifies and loses water-separating capacity; pitting corrosion appears on impellers and bearing inner rings; sludge and varnish build up rapidly, triggering bearing wear, vibration alarms and unplanned shutdowns.
Moisture is a hidden failure source for tropical centrifugal compressors. Anti-corrosion cannot rely solely on coatings. Lubricant selection + system moisture-proof maintenance + shutdown protection must be implemented together. Turbo Compre has developed a complete selection and anti-rust solution based on abundant operational experience from tropical projects.
1. Core Criteria for Lubricant Selection in Tropical High-Humidity Environments
Centrifugal compressor circulating lubrication systems normally adopt R&O (Rust & Oxidation) turbine circulating oil. It differs from screw compressor oil in formulation; hydraulic oil, engine oil and air compressor oil must NOT be mixed for use.
1.1 Base Oil & Viscosity Grade Recommendation
- Priority ranking: Group III hydrotreated base oil (PAO synthetic > Group II hydrotreated > Group I mineral oil). Group I mineral oil oxidizes fast and experiences sharp TAN rise under tropical high temperature with water ingression, not recommended for long-term operation.
- Primary viscosity grade: ISO VG 46 is preferred. VG32 suits cool well-ventilated machine rooms; VG68 is only evaluated separately for heavy-duty gearboxes. ISO VG 46 R&O turbine oil is the top choice for most air centrifugal compressors in tropical conditions, balancing high-temperature oil film strength and low-temperature water separation fluidity.
1.2 Mandatory Oil Performance Indicators for High-Humidity Conditions
- Demulsibility / Water separation: The most critical indicator for humid environments. Fast oil-water separation without persistent emulsification after water ingress. Recommended demulsification value ≤15 min (40-40-0) to avoid continuous corrosion of bearings and rotors by suspended water inside the lube system.
- Anti-rust & anti-corrosion additives: Ashless R&O formulation with vapor-phase corrosion inhibitors and metal passivators. It maintains anti-rust protection during oil film interruption and condensation after shutdown, ideal for intermittently operated units.
- Oxidation stability: Long TOST oxidation life. It restrains TAN growth, varnish and sludge formation under elevated tropical oil temperature, extending oil service intervals.
- Anti-foam & air release properties: High-humidity intake easily generates bubbles. Poor defoaming leads to oil pressure fluctuation and unstable bearing oil supply.
- Seal compatibility: Validated for FKM fluoroelastomer seals to prevent seal corrosion and cavity leakage caused by oil hydrolysis.
1.3 Reference Table for Lubricant Selection
Oil Type | Application Scenario | Advantages & Disadvantages under Tropical High Humidity | Recommended Service Life |
|---|---|---|---|
Group I Mineral R&O Oil | Continuously operated units in dry machine rooms | Low cost; prone to emulsification and fast oxidation, high risk in rainy seasons | 2000~3500 h, shorten sampling interval |
Group II Hydrotreated R&O Oil | Most inland tropical factories | Balanced water separation and anti-rust performance, cost-effective | 4000~6000 h |
PAO Fully Synthetic R&O Oil | Coastal salt spray, intermittent start-stop, high-humidity open-air machine rooms | Best hydrolysis resistance, anti-rust and water separation, withstands frequent condensation | 6000~8000 h |
Selection Warning: Do not use EP extreme-pressure heavy-duty gear oil as main lubricant for centrifugal compressors. EP additives hydrolyze in contact with water and generate acidic substances, accelerating impeller corrosion.
2. System & Structural Rust Prevention Solutions
Lubricant forms a dynamic anti-rust film. However, moisture comes from intake air and chamber condensation after shutdown, so hardware protection is required.
- Intake air dehumidification & filtration: High-efficiency filter, pre-cooling water removal and refrigerated dryer at the inlet cut moisture entering cavities. Add salt spray filter for coastal projects.
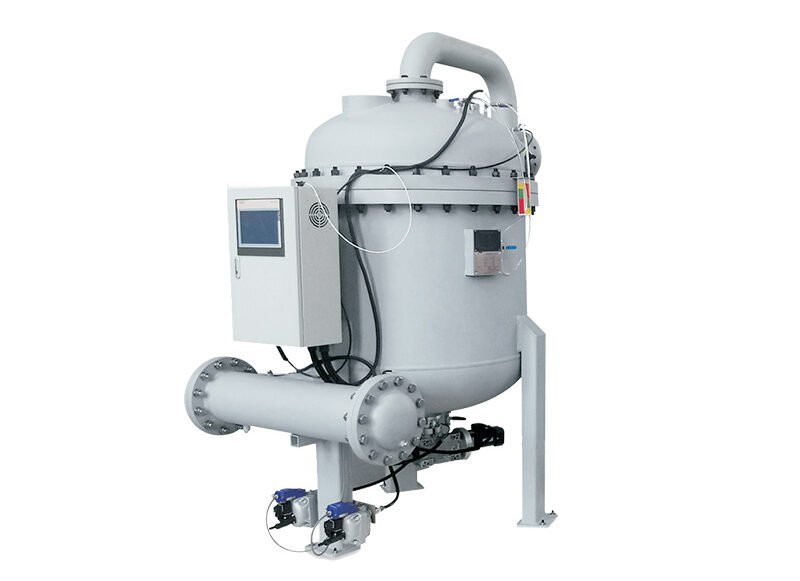
- Oil system dehumidification & drainage: Automatic drain valves plus manual drainage per shift. Electric tracing keeps oil tank 5~8°C above dew point. Vacuum / coalescing dehydrator removes water on-line.
- Cavity positive pressure protection (short-term shutdown): Keep slight dry-air positive pressure after shutdown to block humid air backflow into volutes and impeller passages.
- Long-term shutdown preservation: Over 15 days idle, use nitrogen blanketing; or spray vapor-phase rust inhibitor, fill bearings / gearboxes with preservation oil, seal flanges and inspect regularly.
- Component material & coating: Stainless steel or damp-heat resistant coating for impellers; hydrophobic anti-corrosion coating for cast iron casings.

3. Oil Monitoring & Maintenance Specifications for Tropical High-Humidity Regions
Even premium lubricants fail without periodic testing. Increase sampling frequency under high humidity:
- Sampling cycle: Monthly sampling for continuously running units; biweekly sampling for intermittent operation and coastal salt spray conditions.
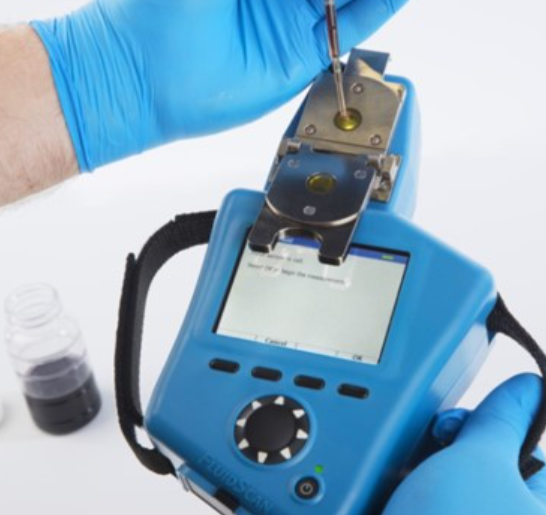
- Mandatory test items: Water content (Karl Fischer), TAN, kinematic viscosity @40°C, demulsibility, rust test, particle count ISO 4406.
- Warning threshold reference:
- Water content >200 ppm: Start oil dehydration; >500 ppm: Shut down for treatment and trace condensation sources;
- TAN rise >0.2 mgKOH/g indicates accelerated oil oxidation, evaluate oil replacement;
- Remarkably prolonged demulsification time means additive depletion and degraded anti-rust performance.
- Maintenance practices: Avoid frequent cold start-stop in rainy seasons. Run under no-load for 30 minutes before shutdown to raise cavity temperature and evacuate residual moisture, then seal after cooling down.
4. Summary of Common Misconceptions
- Misconception: Higher viscosity delivers better rust resistance. → Incorrect. Viscosity shall match bearing design; water separation is the core index for humid conditions. Blind selection of VG68 impairs low-temperature fluidity and drainage.
- Misconception: Oil can keep serving as long as no emulsification is visible. → Incorrect. Dissolved water invisible to the naked eye slowly corrodes bearings and accelerates oxidation.
- Misconception: Continuously running units need no anti-rust treatment. → Incorrect. Condensation forms on inner surfaces once the unit cools down under high ambient humidity. Most impeller passage corrosion occurs during shutdown.
- Misconception: Direct mixing of R&O oils from different brands is acceptable. → Not recommended. Anti-rust additive formulas may conflict and cause demulsification failure and sludge buildup.
For centrifugal compressor rust prevention in tropical high-humidity zones, the core strategy is moisture source control + proper R&O circulating oil selection + closed-loop oil monitoring + shutdown preservation protection. For overseas factories in India, Indonesia and Southeast Asia, ISO VG 46 Group II hydrotreated or PAO fully synthetic R&O turbine oil is the priority recommendation. Matched with oil tank tracing, intake dehumidification and post-shutdown positive pressure protection, it greatly reduces impeller and bearing corrosion failures and extends overhaul intervals.

Turbo Compre is a professional Chinese manufacturer of centrifugal compressors, focusing on R&D, manufacturing and supporting services of complete centrifugal compressor units and spare parts. Targeting the high maintenance cost and long lead time of compressors from international brands, Turbo Compre specializes in interchangeable OEM spare parts matching leading international brands such as Atlas Copco. Our product portfolio covers key components including impellers, main shafts, bearings, gearboxes, oil separators, seals and lube oil systems, supplying highly compatible interchangeable spare parts and complete machine services.