
Turbo Compre 500Nm³/min 8.5barG Skid-Mounted Centrifugal Air Compressor Ready for Delivery

For heavy industries such as chemical, air separation, metallurgy and large chemical fiber, large-flow, high-stability and oil-free clean compressed air serves as the core power guarantee for continuous production lines. With the upgrading of industrial projects toward intelligence, integration and energy conservation, traditional split-type air compressors are plagued by prominent pain points including cumbersome installation, high energy consumption, complicated maintenance and long construction cycles.
To meet the high-end air demand of large-scale industrial projects and solve various challenges of conventional equipment, the 500Nm³/min, 8.5barG high-power skid-mounted integrated centrifugal air compressor independently developed and manufactured by Turbo Compre has successfully completed full-process procedures including assembly, air tightness inspection, load commissioning and factory verification. The unit is fully assembled and ready for shipment to the customer’s site, providing stable, efficient and clean compressed air support for large industrial production.
1. Ultimate Integrated Skid Design, Overhauling Traditional Installation Mode
Most conventional large centrifugal air compressors adopt split designs. Main units, cooling systems, lubrication systems, control modules, pipeline valves and other components are manufactured separately and supplied in split packages. Secondary assembly, pipeline welding, system docking and commissioning must be carried out on site. Such construction mode imposes high requirements for on-site civil engineering conditions, construction equipment and professional technicians. It also brings many drawbacks such as long construction periods, large on-site assembly errors, numerous pipeline joints, high air leakage risk and messy overall layout, greatly raising project construction costs and implementation risks.
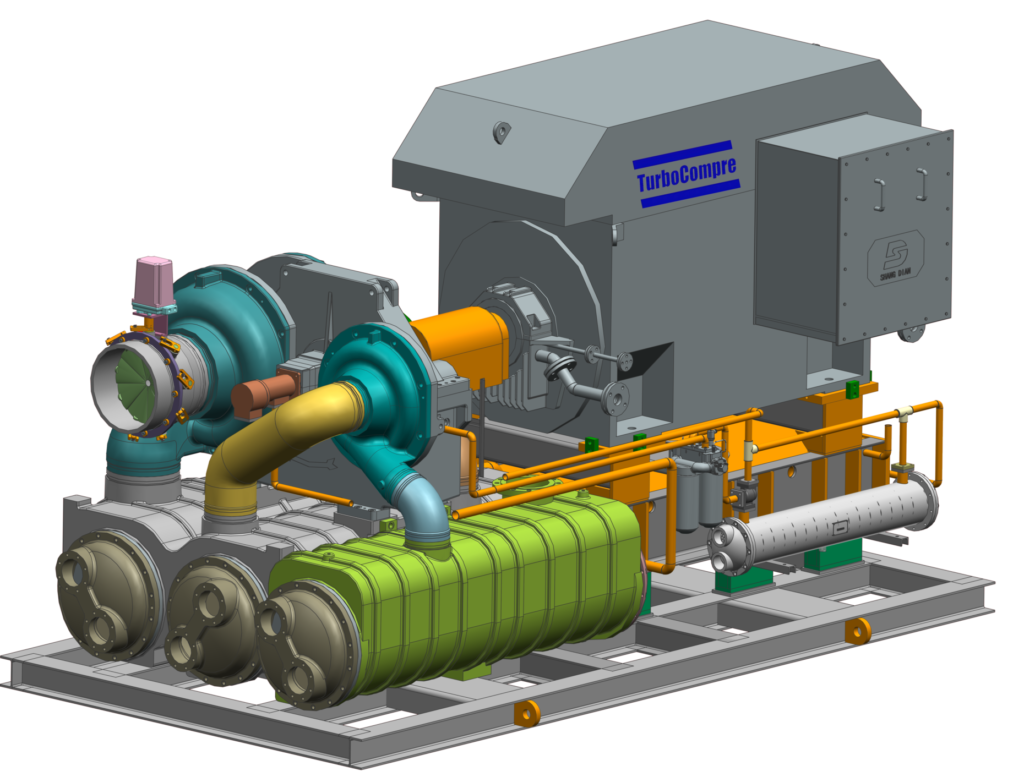
The 500Nm³/min centrifugal air compressor delivered by Turbo Compre adopts an integrated skid-mounted design, fundamentally solving the installation drawbacks of traditional equipment. The core centrifugal mainframe, multi-stage high-efficiency cooling system, intelligent lubrication system, complete pipeline assembly, automatic control system, precision instruments, safety valves and all supporting components are scientifically integrated on an integral steel base frame.

2. Powerful Performance Parameters, Adaptable to Harsh Working Conditions in Large Industries
In terms of core operational performance, this model features large flow, stable pressure and strong adaptability. Its rated gas output reaches 500 standard cubic meters per minute, with stable discharge pressure of 8.5barG. It can continuously supply sufficient and stabilized compressed air around the clock, perfectly matching industrial scenarios with ultra-high air consumption and 24-hour continuous production, such as large air separation units, fine chemicals, metallurgical smelting, chemical fiber polymerization and large pharmaceutical plants.
Relying on Turbo Compre’s independently optimized 3D impeller aerodynamic technology, the main impeller is manufactured by precision casting. Its aerodynamic structure has been optimized through thousands of simulation iterations to minimize air flow loss, and the mainframe efficiency exceeds common models in the industry. Under full-load and variable-load working conditions, the unit can maintain efficient operation, effectively cut power consumption per unit of compressed air.
3. Intelligent & Stable Operation, Low Noise and Long Service Life
Targeting industry pain points of long-term continuous operation, fluctuating working conditions and high failure risks for industrial equipment, Turbo Compre has carried out comprehensive upgrades on this model. The complete unit adopts a high-strength frame structure optimized by professional vibration simulation, paired with high-precision dynamic balance calibration technology. The unit generates extremely low vibration during operation, avoiding common problems of large units such as excessive vibration, component wear and abnormal noise. Meanwhile, it is equipped with professional noise reduction and sealing structures. The operating noise is strictly controlled within environmental protection standards, suitable for modern green factory construction.
For intelligent control, the unit is equipped with Turbo Compre’s self-developed full-automatic intelligent control system. It monitors core operating parameters including unit pressure, flow rate, temperature, vibration and oil pressure 24/7.

4. Convenient Maintenance Design to Reduce Enterprise Operating Costs
The maintenance convenience of large industrial equipment directly determines the long-term operating cost of enterprises. At the product design stage, Turbo Compre fully considers the practical needs of later inspection, maintenance and spare parts replacement. The overall layout of the unit is scientifically planned with sufficient and regular maintenance space reserved. Core wearing parts such as impellers, bearings, seals and instrument valves are easy to disassemble without complicated tools and tedious operations, greatly lowering daily maintenance difficulty and labor costs.
Furthermore, the intelligent control system can automatically store operation data, record fault information and generate maintenance reminders. It helps maintenance personnel accurately grasp equipment status and realize predictive maintenance and refined management. It completely changes the traditional mode of“repair after failure and blind maintenance”, effectively extending equipment service life and reducing failure rate, so as to safeguard stable operation of production lines.

5. Core Advantages of Turbo Compre: Technology Oriented, Service Empowered
As a high-end manufacturing enterprise in China’s centrifugal compressor sector, Turbo Compre has been deeply engaged in this industry for years. It focuses on the R&D, design, production and sales of centrifugal air compressors, centrifugal blowers and other high-end fluid equipment, accumulatingprofound technical know-how and rich practical project experience. Compared with peers, it has multiple core competitive strengths:
- Independent Core Technology & Customization: Boasting a professional R&D team, Turbo Compre independently masters core technologies such as 3D impeller design, aerodynamic optimization, intelligent control and skid integration. It provides one-to-one customized equipment solutions tailored to customers’ actual working conditions, air demand and site conditions, avoiding homogeneous products and perfectly adapting to diverse industrial needs.
- Full-process Precision Quality Control: Equipped with standardized workshops and professional precision testing equipment, Turbo Compre implements a strict full-process quality inspection system covering raw material procurement, component processing, assembly, testing and factory verification. Every unit undergoes rigorous inspections to ensure outstanding stability, reliability and durability.
- Rich Cross-industry Project Experience: Turbo Compre’s products are widely applied in chemical, air separation, metallurgy, pharmaceutical, new energy and other core industries. Serving numerous domestic and overseas enterprises, the brand has rich experience in large-flow centrifugal unit projects and delivers reliable solutions for complex and harsh working conditions.

- Full-cycle One-stop After-sales Service: Differing from conventional equipment suppliers, Turbo Compre offers a full-chain service system including scheme design, customization, manufacturing, commissioning, on-site guidance, technical training and lifelong maintenance. The professional team provides rapid after-sales response, ensuring worry-free purchase and operation for all customers.